Hey there, Semi-Automatic Band Saw

Let’s cut to the chase—if you’ve ever wandered the metal fabrication floor, you’ve probably stared at a semi-automatic band saw and wondered, “Can this thing actually handle non-ferrous metals? Like aluminum, copper, brass, or even that weird soft alloy someone hauled in last week?” I get it. For years, I fielded this exact question at our shop (the one where I’ve been selling and tweaking these saws for 12 years) so trust me, this isn’t some random internet take. This is stuff I’ve seen work, and stuff I’ve seen go sideways when folks don’t set things right.
First, let’s nail down what a semi-automatic band saw actually is, quick—no boring manual, I promise. Unlike the old manual ones where you yank the arm down with all your might, semi-auto means you push a button to start the blade, it feeds at a consistent (adjustable) speed and pressure, and it stops automatically when your cut’s done. No cranking, no guessing how hard to push. That’s the key here, because non-ferrous metals are weirdly specific—soft, gummy, some have that tendency to grab the blade or “gum up” the teeth if you mess with how you run the saw.
Now, the big question: can it work? Short answer—hell yeah, it can. But let’s not act like it’s plug-and-play, okay? I’ve seen guys show up with a pile of 2-inch thick aluminum bars, hook up their basic semi-auto, and walk away with perfectly square, burr-free cuts. I’ve also seen them try to cut 1-inch solid copper with the wrong blade, crank the feed too high, and end up with a blade that snapped mid-cut (that was a $800 blade, by the way—they weren’t happy). So it’s less about the saw itself and more about how you pair the saw with the metal, the blade, and your settings.
Let’s break down the non-ferrous stuff first because they’re not all the same. Soft stuff like aluminum and brass are the most common culprits here. They’re ductile, so they don’t chip like steel—they kind of squish and stick to the blade teeth. That’s where a semi-auto’s consistent feed rate saves your ass. Manual saws? You might push too hard, which makes the metal squish, clog the teeth, and cause that terrible chatter (you know the sound—high-pitched, like a fingernail on a chalkboard, and it ruins your cut). Semi-auto keeps that feed steady, so the blade bites clean without mashing the metal. I’ve cut 4-inch thick 6061 aluminum on our entry-level semi-auto last month for a bike frame shop—came out so clean they didn’t even need sanding.
Copper is trickier. It’s super soft and gummy—think of cutting a warm candy bar, that’s what copper feels like sometimes. If your semi-auto can’t adjust the feed to be slow and steady, you’ll just drag the blade through it, not cut. I learned this early on—we had a customer who tried cutting ½-inch copper tubing on a cheap entry-level semi that only had three feed settings. He picked “medium” and the blade just sat there melting a groove into the tubing, not cutting. Switched to our mid-tier semi with infinite adjustable feed, set it to 12 SFPM (surface feet per minute, for the nerds), and it zipped through it like butter.
What about the other side—what’s holding people back from using semi-auto band saws for non-ferrous? I think a lot of it is old hype that band saws are only for steel. That’s garbage. Steel is hard, so it needs aggressive teeth, non-ferrous need different teeth. The blade is the biggest variable, not the saw. You can’t use a bi-metal blade meant for cutting 1-inch solid steel to cut 2-inch aluminum. You need a blade with more, smaller teeth—like 10-14 TPI (teeth per inch) for most non-ferrous. Wait, no—wait, thin stuff like ¼-inch aluminum sheet? You want 18-24 TPI so the teeth don’t skip. Thick stuff like 4-inch aluminum? 6-10 TPI, because the bigger teeth clear the gummy chips faster. I can’t tell you how many guys swap the wrong blade and then blame the saw. The semi-auto is just the tool that lets you use that blade correctly.
Another thing semi-autos do better than manual: they handle the clamping pressure. Non-ferrous metals are soft, so if your clamp is too loose, the part will move mid-cut, ruin it. Too tight? You’ll deform the metal, bend it. Semi-automatic band saws have hydraulic or pneumatic clamping that’s adjustable, so you can dial it in just right. I watched a fabricator last week cut 12 brass valve bodies—each was a weird, irregular shape, nothing to clamp evenly on. He used our semi-auto’s custom vise inserts, set the clamp pressure to just enough to hold it without squishing, and all 12 cuts were spot-on. A manual saw would’ve required 3 extra guys holding the parts, and half of them would’ve been ruined.
Wait, let’s talk about the downsides, because I don’t want to paint a perfect picture. Semi-autos cost a little more than manual, right? But think about what you’re saving: less blade breakage, fewer ruined parts, no wasted time cranking a manual arm for 10 cuts. For a small shop doing 20 non-ferrous cuts a day, that extra cost pays for itself in a month. Also, if you’re cutting really thin, flimsy non-ferrous—like 18-gauge aluminum sheet—you might need a semi-auto with a variable speed that can go super slow. Some basic entry-level semi-autos max out at 100 SFPM, which is too fast for thin sheet. But that’s not the saw’s fault, that’s buying the wrong saw for the job. I always tell customers: tell me what you’re cutting, how often, and how thick, and I’ll point you to the right semi-auto. No one-size-fits-all.
Let’s get real about a common mistake I see: people use the same coolant for steel and non-ferrous. Wait, when cutting non-ferrous, you need a coolant that’s not going to react with the metal. Straight cutting oil works great for copper or brass, because it lubricates and keeps the gummy chips from sticking to the blade. For aluminum, a water-soluble coolant that’s non-corrosive is better—rust is bad, but aluminum corrosion is way worse, and it’ll ruin your parts if you leave that residue. Semi-automatic band saws usually have a built-in coolant pump, which is a huge upgrade over manual ones where you have to spray a bottle of WD-40 every 2 cuts. That’s consistent coolant, every time, no work.
I’ve had a lot of customers come to me after switching their non-ferrous cutting over to semi-autos, and they say the same thing: “I didn’t know this was possible.” One guy runs a custom sign shop—he used to use a jigsaw for all his aluminum trim, which left burrs and took twice as long. Got our entry-level semi-auto, set it up for ⅛-inch sheet, runs it at 150 SFPM, and now he cranks out 50 cuts in the time he used to do 10. No more sanding edges, no more jigsaw blades snapping every 5 cuts. That’s the real win here—productivity.
Wait, what about exotic non-ferrous? Like titanium? Wait no, titanium is technically non-ferrous, but it’s hard, so you’d use a different blade and slower speed. But even that works on a semi-auto—you just dial the feed down, use a 14 TPI carbide-tipped blade, and it cuts through titanium like it’s tough steel. I wouldn’t try that on a basic entry-level semi if you’re running titanium every day, but our mid-tier or industrial semi-autos? Total game-changer for those high-end parts.
Let me circle back to the original question because I don’t want to ramble. Can a semi-automatic band saw be used for cutting non-ferrous metals? Yes, but only if you do it right. It’s not a “set it and forget it” thing—you have to pair the right blade, adjust the feed speed, clamp pressure, and coolant for the specific non-ferrous metal you’re cutting. But if you do that, it’s way better than manual saws, better than jigsaws or chop saws, and way more consistent.
Here’s the thing: I’m not just selling saws. I’m a guy who’s been in this game for over a decade, fixing saws, troubleshooting bad cuts, and watching guys make money or lose it based on their tools. The biggest mistake people make is assuming a saw is only for one type of metal. A good semi-automatic band saw is versatile—you can cut steel, stainless, aluminum, brass, copper, all with the right setup. You just have to know how to adjust it, and that’s what I help with.
If you’re tired of dealing with ruined non-ferrous cuts, broken blades, or wasting time on manual saws that can’t keep up, let’s talk. No pushy sales pitch, no weird jargon. I’ll ask what you’re cutting, how much, and point you to the semi-auto that works for your shop—even if it’s not one of ours, honestly. But if it is, we’ll make sure you’ve got the blades, the coolant, and the tips to get the job done right. Because at the end of the day, your cuts are my cuts.
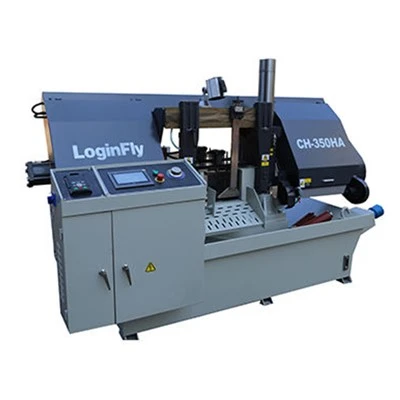
Don’t overcomplicate this stuff. Semi-automatic band saws are totally capable of handling non-ferrous metals—you just have to stop thinking they’re only for steel, and start adjusting your setup for the metal you’re working with. It’s not rocket science, it’s just common sense paired with a tool that does the work for you.
Metal Cutting Band Saw References:
- "Metalworking Band Saw Blade Selection Guide", Modern Machine Shop, 2022.
- "Cutting Non-Ferrous Metals Safely and Efficiently", Fabricator Magazine, 2021.
- "Semi-Automatic Band Saw Operational Best Practices", SME Metalworking Handbook, 2020.
Shanghai Loginfly Sawing Technology Co., Ltd.
As one of the most professional semi-automatic band saw manufacturers and suppliers in China, our products have good reputation in the market. We warmly welcome you to wholesale premium semi-automatic band saw from our factory. If you have any enquiry about cooperation, please feel free to email us.
Address: Room 506 NO.655 Yinxiang Road,Nanxiangtown,Jiading District, Shanghai.China
E-mail: sales01@loginfly.com
WebSite: https://www.loginflysaws.com/
